Battery manufacturing is entering a sharper, less forgiving phase. The International Energy Agency reported that global battery demand for electric vehicles reached about 750 GWh in 2023. It also expects demand to expand significantly this decade. More cells mean more pressure on yield, speed, safety, and material efficiency.
This is where laser processing becomes practical, not decorative. How does laser cutting improve battery manufacturing? It creates precise electrode shapes, narrow kerfs, clean tabs, and repeatable edges. These details matter when a small burr can damage a separator or trigger an internal short circuit. Laser systems also support high-speed production, digital control, and reduced mechanical contact. Less contact can mean less tool wear and fewer contamination risks. Sometimes, the smallest edge decides the largest loss.
Dr. Heiner Heimes of RWTH Aachen University has emphasized the manufacturing challenge: “Battery production requires high-quality processes with stable and reproducible results.” That principle explains laser cutting’s growing role. BloombergNEF’s 2024 Battery Price Survey placed the average lithium-ion battery pack price at 115 dollars per kWh, showing how strongly manufacturers must control waste and cost. The U.S. Department of Energy also identifies manufacturing quality and process innovation as important priorities for a competitive battery supply chain. Still, lasers are not a universal cure. Reflection, thermal damage, equipment cost, and imperfect parameter settings remain real concerns. The following top ten methods examine where laser cutting delivers measurable value—and where manufacturers should remain cautious.
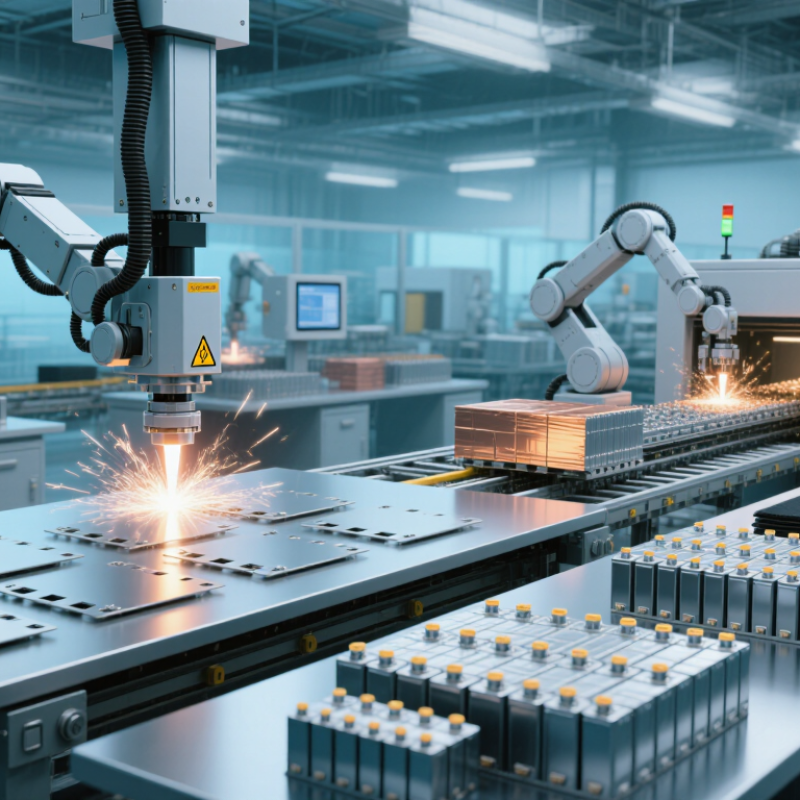
Electrode Preparation: Sub-100 µm Kerfs Improve Edge Quality and Material Yield
Top 10 Ways Laser Cutting Improves Battery Manufacturing?
Electrode preparation depends on clean, repeatable cutting. A sub-100 µm kerf removes less active coating between adjacent parts. This can improve material yield, especially on expensive coated foils. It also produces narrower edges, reducing loose particles and uneven current paths. The result is more usable electrode area inside each cell.
The scale is significant. The International Energy Agency reported global electric-vehicle battery demand reached about 750 GWh in 2023, rising nearly 40% year over year. At this volume, small cutting losses become expensive. BloombergNEF’s 2024 Battery Price Survey placed average lithium-ion pack prices at 115 dollars per kWh. Every saved millimeter deserves measurement.
Clean edges matter.
A focused laser can create precise tabs, notches, and contours without mechanical blade wear. Operators should inspect heat-affected zones, burrs, and debris after every process change. A narrow kerf alone does not guarantee quality. Excessive energy can damage the coating or create microscopic cracks. That is the uncomfortable part: yield gains require process validation, not optimistic specifications. Inline vision, kerf checks, and periodic electrical testing help connect cutting accuracy with actual cell performance.
Sources: IEA, Global EV Outlook 2024; BloombergNEF, Battery Price Survey 2024.
Cell Assembly: ±10 µm Tab Cutting Enhances Alignment and Weld Consistency
In cell assembly, tab geometry often decides whether a weld starts cleanly. Laser cutting within ±10 µm keeps each tab close to its programmed position. That narrow tolerance helps electrode stacks meet busbars without forced adjustment. Less repositioning means fewer wrinkles, tilted tabs, and uneven contact pressure. The improvement is visible at the fixture: tab edges line up under the welding head instead of drifting across the clamp.
Consistent edges also support weld consistency. A stable overlap gives welding energy a repeatable path and reduces skipped spots or excessive penetration. Operators can monitor cut width, burr formation, and heat-affected zones through scheduled inspections. Vision systems should verify every critical dimension, not merely sample a few cells. Clean optics, calibrated stages, and controlled assist gas matter too. Small maintenance gaps can quietly erase a ±10 µm advantage.
Still, tight cutting accuracy cannot repair poor stack alignment upstream. Material spring-back, fixture wear, and foil variation may remain. We have seen promising first runs weaken after extended production. Process records should connect cut data with weld resistance, pull strength, and defect location. A practical trial might compare tabs after 10,000 cycles, not only after setup. The target is not perfect numbers. It is repeatable assembly under changing conditions.
How ±10 µm Laser Tab Cutting Supports Battery Cell Assembly
A smaller tab-position tolerance leaves more alignment margin for ultrasonic or resistance welding.
The ±10 µm target reduces the maximum positional deviation by 60% versus ±25 µm and by 80% versus ±50 µm, helping maintain consistent tab overlap and weld placement.
Values represent engineering tolerance scenarios; lower deviation indicates tighter cutting control.
Throughput: Noncontact Processing Reduces Tool Wear Across 1,000+ Cycles
Top 10 Ways Laser Cutting Improves Battery Manufacturing
Throughput is one of laser cutting’s clearest advantages in battery production. Noncontact processing avoids blade contact with electrode films, tabs, and separator edges. That reduces tool wear across 1,000+ cycles. It also limits interruptions caused by sharpening, replacement, and mechanical alignment.
In a well-tuned line, the beam follows programmed paths at consistent speed. Operators can inspect narrow kerfs, clean edges, and stable part dimensions during scheduled checks. Fewer tool changes may improve throughput and simplify production planning. Less physical pressure can also reduce deformation in thin materials. Small details matter here.
However, laser cutting is not automatically perfect. Excessive energy may create heat-affected zones, residue, or rough edges. These defects can affect downstream stacking and electrical performance. Experienced technicians should verify pulse settings, focus position, extraction, and material thickness. They should also sample parts after extended runs, not only at startup. A 1,000-cycle result can look impressive, yet maintenance records may reveal gradual contamination or calibration drift. That is where honest review matters. Throughput gains should be measured with inspection time, rejected parts, and actual uptime included.
Safety and Quality: Burr-Free Edges Lower Risks of Shorts and Contamination
Laser cutting improves battery manufacturing by producing precise, burr-free edges on foils, tabs, and thin metal sheets. These clean edges reduce sharp projections that can pierce separators during stacking or winding. That matters because a tiny metal fragment can create an internal short circuit.
Cleaner cutting also limits loose particles around the cell. Copper and aluminum dust may settle on active materials, bonding surfaces, or insulation films. Controlled laser parameters can reduce this debris and support cleaner workstations. Operators should still use extraction systems and scheduled particle checks. Cutting alone cannot remove every contaminant.
The process can maintain tight dimensions across repeated parts. Consistent tab shapes improve alignment during assembly and reduce unnecessary pressure on nearby layers. In production reviews, edge quality should be checked under magnification, not judged by appearance alone. Microscopic burrs may remain invisible to the naked eye.
Still, laser cutting is not automatically perfect. Excessive energy can create heat-affected zones, discoloration, or minor melting. Insufficient energy may leave incomplete cuts and fragile edges. Engineers need to balance power, speed, focus, and assist gas for each material thickness. Sampling after tool changes is wise. A burr-free edge is valuable, but only when inspection confirms it.
Smart Manufacturing: Inline Laser Inspection Supports 100% Traceability
Laser cutting improves battery manufacturing by creating clean, repeatable edges on foils, tabs, and casing materials. However, cutting accuracy alone is not enough. Inline laser inspection checks every component as it moves through production. It measures edge position, hole diameter, burr size, and surface damage within milliseconds. Each result can link to a batch, machine setting, and timestamp. This creates 100% traceability instead of relying on occasional manual sampling.
In practice, inspection data helps engineers find process drift early. A changing laser focus may create wider kerfs or rougher edges. The system can flag these defects before they reach cell assembly. Operators can review images beside measurement values, making decisions faster and more defensible. Still, inspection is not magic. Dust, vibration, reflective materials, and poor calibration can produce false alarms. Human review remains important, especially when unusual defects appear.
Tips: Keep inspection records connected to cutting parameters, not stored separately. Calibrate cameras and laser sensors on a fixed schedule. Define clear limits for burrs, offsets, and incomplete cuts. Test the system with known defects, including small defects that operators might miss. Review false rejects every week. They may reveal poor thresholds, unstable lighting, or a deeper production issue. Reliable traceability depends on disciplined data handling, not just advanced equipment.
FAQS
It keeps tab edges near their programmed positions. Cleaner alignment follows. Tabs meet busbars with less forced adjustment. This reduces wrinkles, tilted tabs, and uneven contact pressure.
Yes, stable overlap gives welding energy a repeatable path. It can reduce skipped spots and excessive penetration. Operators should still check weld resistance and pull strength. Cutting accuracy alone cannot guarantee strong welds.
Vision systems should verify every critical tab dimension. They can check cut width, burrs, edge position, and heat-affected zones. Sampling only a few cells may miss gradual drift. That is an uncomfortable weakness.
Clean optics, calibrated stages, and controlled assist gas are important. Operators should inspect residue and focus position regularly. Small maintenance gaps can erase a ±10 µm advantage. The machine may look stable while accuracy quietly declines.
The beam does not physically press against films, tabs, or separator edges. This reduces blade wear and interruptions from sharpening or replacement. Thin materials may also experience less deformation. Fewer tool changes can simplify production planning.
Not always. Extended operation may reveal contamination, calibration drift, or gradual edge changes. Reviews should include inspection time, rejected parts, and actual uptime. A strong early result can weaken later.
Excessive energy may produce heat-affected zones, residue, or rough edges. These defects can disturb stacking and electrical performance. Technicians should verify pulse settings, focus position, extraction, and material thickness. More energy is not automatically better.
They should connect cutting data with weld resistance, pull strength, and defect locations. Trials should examine parts after extended production cycles, not only after setup. Fixture wear, foil variation, and material spring-back still matter. Perfect numbers are not the real target. Repeatable assembly is.
Conclusion
Laser cutting is transforming battery manufacturing by improving precision, productivity, and process control across multiple stages. In electrode preparation, sub-100 µm kerfs create cleaner edges, reduce material waste, and support more consistent active-layer dimensions. During cell assembly, tab cutting accuracy of approximately ±10 µm improves component alignment and helps create more reliable, uniform welds. Because the process is noncontact, it minimizes tool wear and maintains stable performance over more than 1,000 processing cycles, reducing downtime and maintenance needs.
So, how does laser cutting improve battery manufacturing? It produces burr-free edges that lower the risk of internal shorts, contamination, and handling defects while supporting safer, higher-quality cells. When combined with inline laser inspection, manufacturers can monitor dimensions and cutting quality in real time, identify deviations early, and maintain complete traceability for every production unit. Together, these advantages enable more efficient material use, stronger process consistency, and scalable smart manufacturing.
 Stylo Laser